

GEARCASE
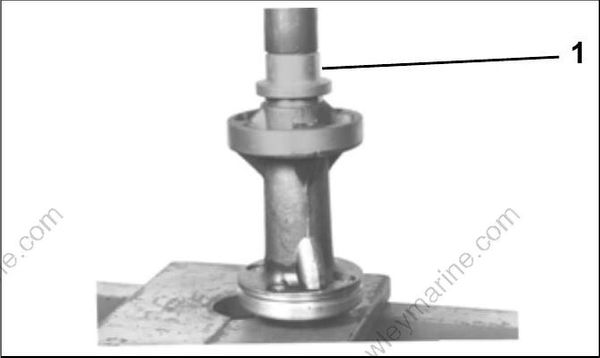
Rear Bearing
- Bearing installation tool
Rear Seal Installation
Install new seals back to back in bearing housing using Seal Installer, P/N 326551. Apply Gasket Sealing Compound to metal casings of the seals before installing.
Install inner seal with lip facing toward the bearing housing, then outer seal with lip facing away from the bearing housing.
Apply Triple-Guard grease to seal lips.
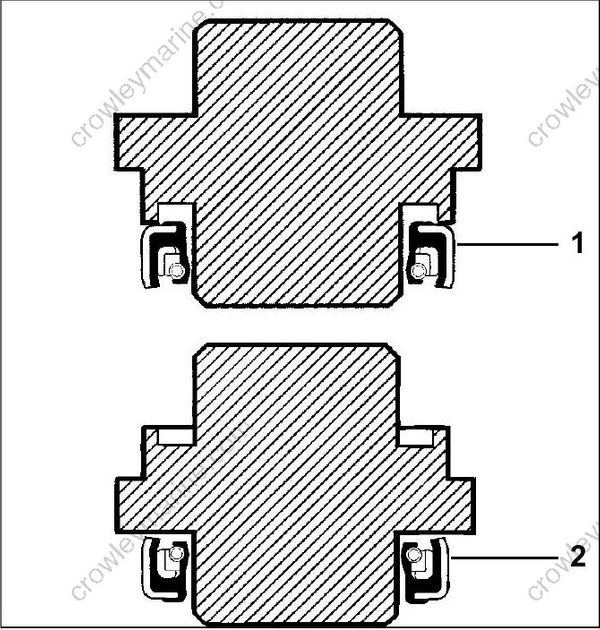
- Inner seal
- Outer seal
DRIVESHAFT SHIMMING
IMPORTANT: If new pinion gear is needed, replace gear set before shimming procedure.
Pinion gear backlash is achieved by using shims between the driveshaft bearing housing and the thrust washer. When installing a new thrust bearing or washer, bearing housing, pinion, or drive shaft, it is necessary to properly shim the assembly to restore factory clearance.
Use Driveshaft Shimming Tool, P/N 393185.
Shim gauge bars are precision made and should be handled carefully. The length of each bar is stamped near the part number. This dimension is 0.020 in. (0.508 mm) shorter than the actual shimmed length of the driveshaft.
IMPORTANT: Degrease pinion and driveshaft tapers prior to assembly. Check tapers for any damage or material transfer. Replace any damaged components before proceeding.
Assemble the driveshaft bearing housing, thrust washer, thrust bearing, and pinion onto the drive shaft. Use Driveshaft Seal Protector, P/N 312403, whenever installing or removing the bearing housing. Lightly coat the threads of the pinion nut with outboard lubricant and torque to 40 to 45 ft. lbs. (54 to 60 N·m).
IMPORTANT: The original pinion nut may be used for shimming, but must NOT be used in final assembly.
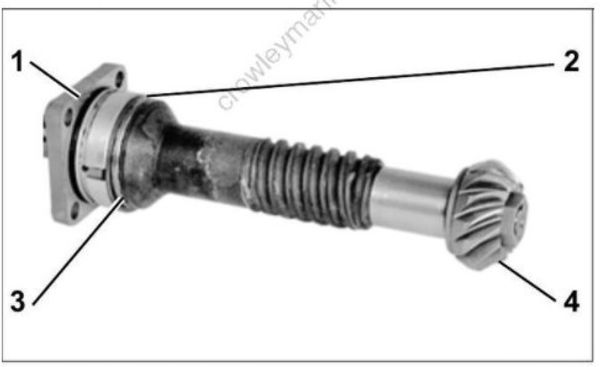
- Driveshaft bearing housing
- Thrust washer
- Thrust bearing
- Pinion
Select Collar, P/N 328363, and Shim Gauge Bar, P/N 328366.
Slide the collar onto the driveshaft with large end in contact with the bearing housing.
Insert the assembled driveshaft into the tool base and tighten preload screw against the driveshaft until groove on the spring-loaded plunger is flush with end of threads. Tighten locking ring on preload screw.
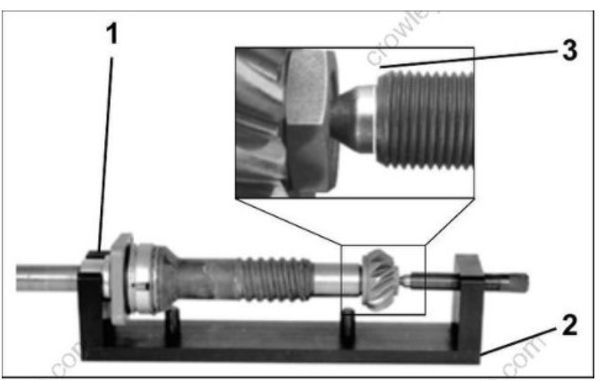
- Collar
- Tool base
- Groove
Rotate the driveshaft several revolutions to seat bearings.
Lay the tool base on its side. Position the shim gauge bar against guide pins of the tool base.
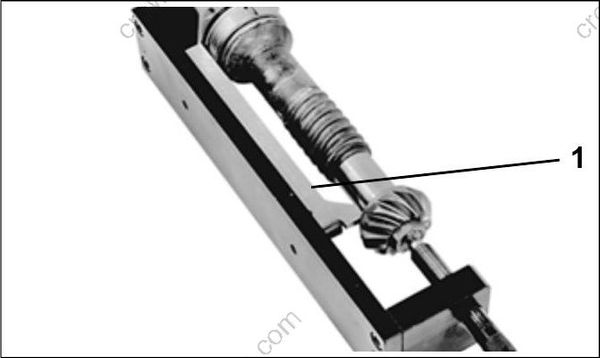
- Shim gauge bar
Check the squareness of the bearing housing mounting surface by holding the shim gauge bar against the pinion while rotating just the bearing housing and measuring the clearance between the gauge bar and the bearing housing with feeler gauges. Measure between each pair of screw holes. Replace the bearing housing and repeat check if variance exceeds 0.004 in. (0.010 mm).
Check the squareness of the pinion to the driveshaft by holding the shim gauge bar against the bearing housing (between the screw holes) while rotating just the driveshaft and pinion assembly and measuring the clearance between the shim gauge bar and the pinion. Replace the pinion or the driveshaft, as necessary, and repeat the check if variance exceeds 0.002 in. (0.050 mm)
Subtract the average clearance measurement you obtained from 0.020 in. (0.508 mm) to determine the correct shim thickness required. Select the fewest number of shims to achieve the correct thickness.
Remove the driveshaft from the tool base. Remove the collar and bearing housing from the driveshaft, and add the required amount of shims.
IMPORTANT: Use extreme care when removing bearing housing to avoid damaging the seals. Use Driveshaft Seal Protector, P/N 312403.
Check shimming by reassembling the driveshaft with shims and placing it back into the tool base. The measurement between the gauge bar and the pinion should be 0.020 in. (0.508 mm).
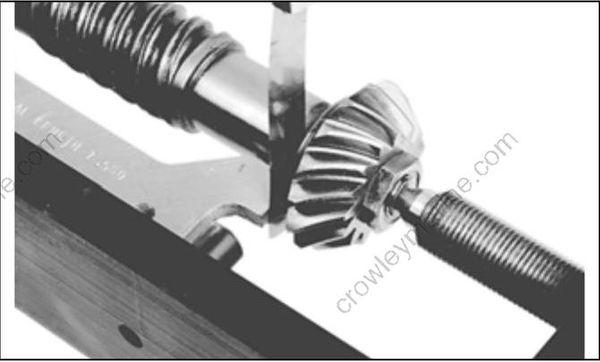
Remove the nut and pinion from the driveshaft.
Discard the nut.
