

POWERHEAD INSPECTION
For dimensions, refer t o SERVICE SPECIFICATIONS on p. 10.
IMPORTANT: Before any inspect ion process can begin, all internal components must be completely clean and free of contaminants.
Visually inspect all parts. Check for unusual wear patterns, scuffing, or deterioration of aluminum parts, heat-related discoloration of bearings a nd
bearing surfaces, and broken components.
Cylinder Head
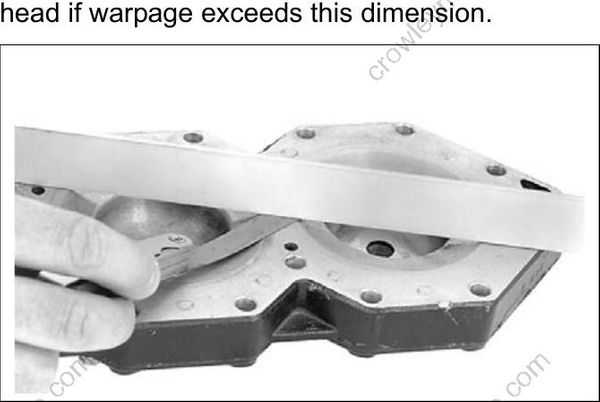
Check for cylinder head warpage using a piece of bar stock or machinist’s straightedge and a feeler gauge set.
Cylinder head warpage must not exceed 0.006 in. (0.15 mm) per inch of measurement. Re place head if warpage exceeds this dimension.
24423
Check fuel deflector pins for damage.
Crankshaft
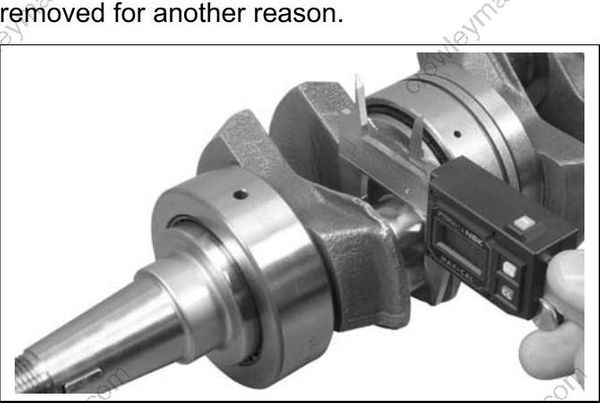
Measure the diameter of each crankpin and main bearing journal. The lower main bearing journal would only be measured if the bearing was removed for another reason.
002142
Cylinder Bore
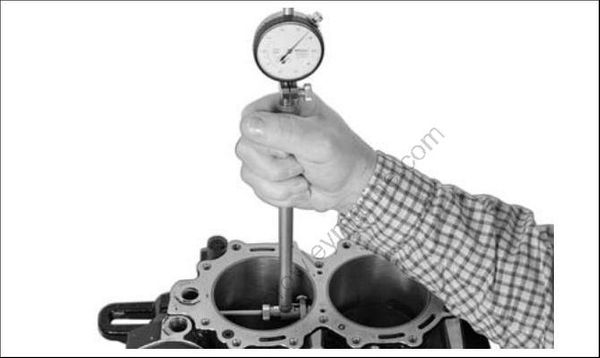
Use a Cylinder Bore Gauge to inspect each cylinder bore for an out-of-round, oversize, or tapered condition. Be sure the gauge is perfectly square in the bore when measuring.
007283
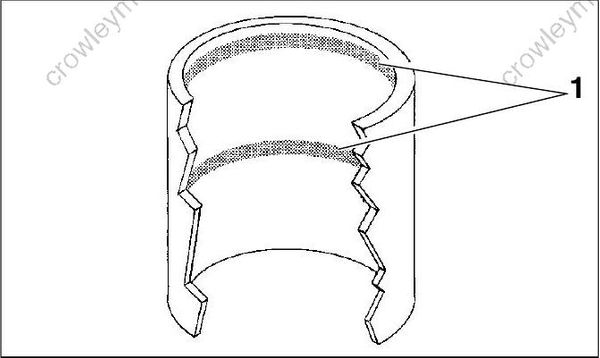
Measure each cylinder in at least two areas. Each area should b e measured twice. The difference between the two measurements in each are a is
the cylinder out-of-round dimension.
• The cylinder must not be out-of-round by more than 0.004 in. (0.10 mm).
The dimensional difference between the two areas is cylinder taper.
• The cylinder taper must not exceed 0.002 in. (0.05 mm).
- Measurement areas DR3482
The difference between the measurement s and standard bore is cylinder oversize. For dimensions, refer to SERVICE SPECIFICATIONS on p. 10.
• The cylinder must not be oversized by more than 0.003 in. (0.08 mm).
Pistons
Visually inspect pistons for sign s of abnormal wear, scuffing, cracks, or burning.
Piston Rings
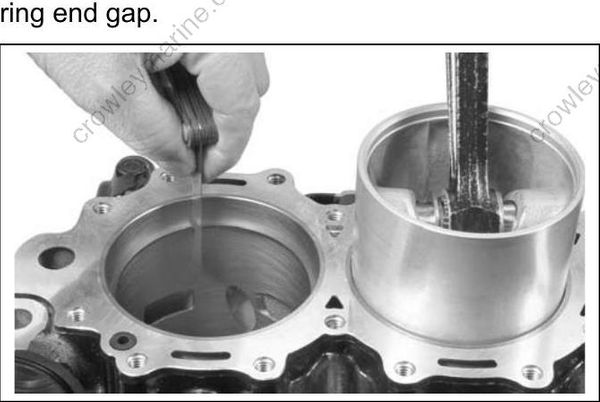
For new ring sets, place each ring separately in its respective bore. Use a piston to square the ring in the cylinder. Use a feeler gauge to measure the
ring end gap.
002143
Ring end gap should be:
• 0.011 to 0.023 in. (0.28 to 0.58 mm)
IMPORTANT: Ring end gap increases approximately 0.003 in. (0. 076 mm) for each 0 .001 in. (0.025 mm) increase in cylinder bore diameter. DO NOT exceed cylinder oversize dimension.
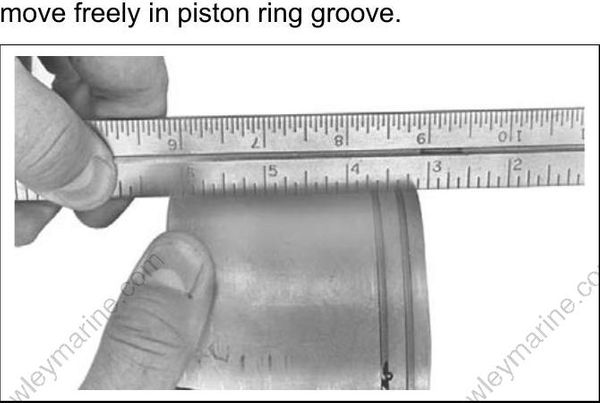
Use a machinist’s straightedge to check for proper ring clearance. Position piston rings o n piston. Push rings into groove and hold straightedge against the side of the piston. Rings must be even or just be low the surface of piston . Rings must move freely in piston ring groove.
31796
Bearings
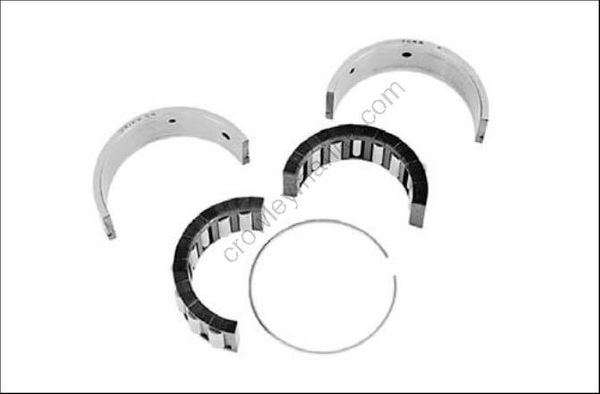
Inspect center main bearings and split sleeves for excess wear, nicks, or scratches. Replace if necessary.
Inspect crankshaft rod bearings for excess wear, nicks, or scratches. Replace if necessary.
24381
