

ASSEMBLY
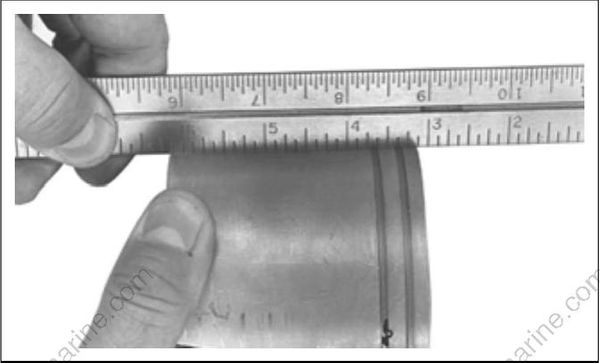
or just below the surface of piston. Rings must move freely in piston ring groove.
31796
Bearings
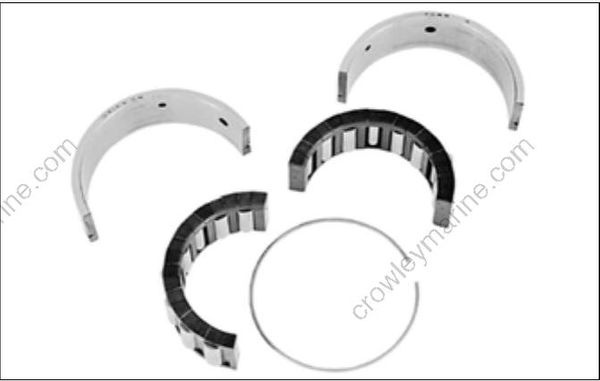
Inspect center main bearing and split sleeves for excess wear, nicks, or scratches. Replace, if necessary.
24381
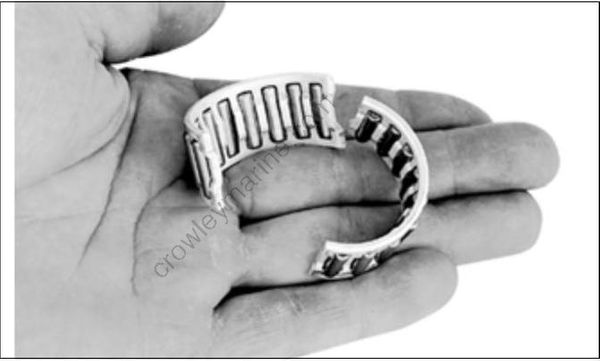
Inspect crankshaft rod bearings for excess wear, nicks, or scratches. Replace, if necessary.
24377
ASSEMBLY
IMPORTANT: Proceed slowly. Make no forced assemblies unless a pressing operation is called for. All internal components must be perfectly clean and lightly coated with outboard lubricant.
IMPORTANT: Use new wrist pin retaining rings, gaskets, seals, and O-rings during assembly.
Crankshaft
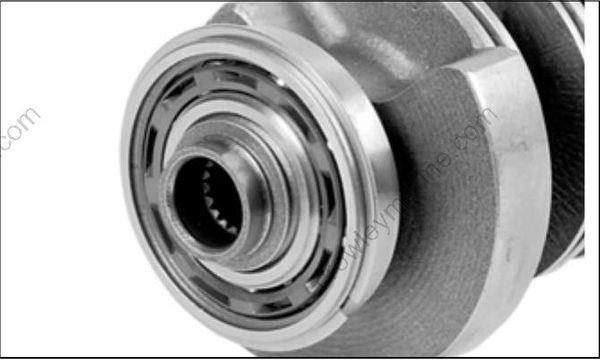
Oil the end of the crankshaft. Use Crankshaft Bearing/Sleeve Installer, P/N 338647, and place a new lower main bearing onto crankshaft with lettered side facing the tool. Install bearing until it seats on the crankshaft.
29020
Oil the end of the crankshaft. Place a new sleeve in the Crankshaft Bearing/Sleeve Installer, P/N 338647, and drive the sleeve onto the crank shaft until the installer contacts the lower main bearing.
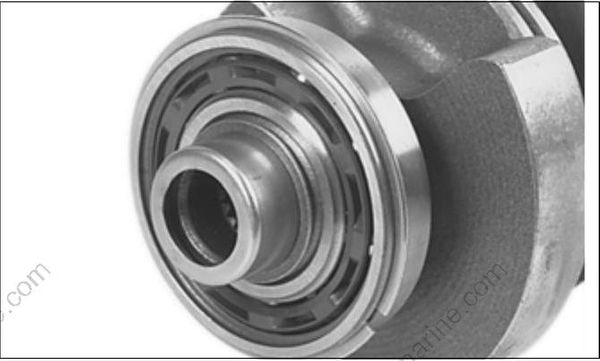
29021
If the installer sticks on the sleeve after installation, thread Slide Hammer, P/N 391008, into installer and pull it off.
IMPORTANT: Inspect sleeve after installation. Sleeve must not be used if surface is damaged.
Using retaining ring pliers, install bearing retaining ring with sharp edge facing away from bearing.
Lubricate a new driveshaft O-ring and lightly lubricate crankshaft splines with Moly Lube Install O-ring in sleeve.
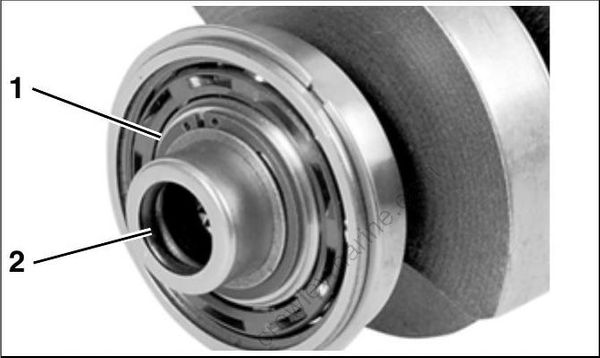
- Bearing retaining ring 29022
- O-ring
Lubricate the center main bearings and split sleeves with outboard lubricant and install them in their original positions. The split sleeve ring grooves must face toward driveshaft (lower) end of crankshaft when installed.
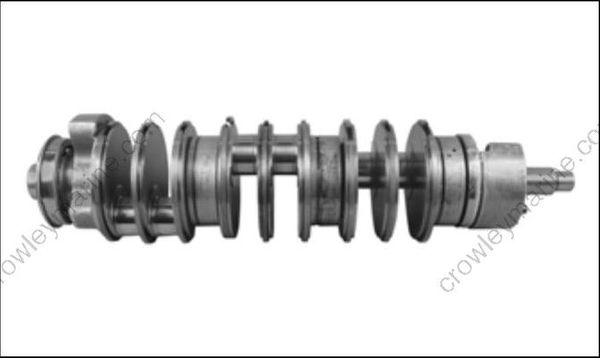
005282
Lightly coat the metal case of a new lower housing seal with Gasket Sealing Compound. Press against outer metal case of the seal and install seal in the lower housing with extended lip of seal
ASSEMBLY facing down. The seal lip faces the bottom of the crankshaft.
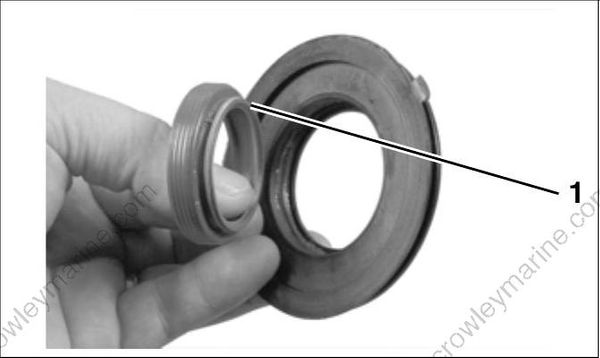
- Extended lip 002036
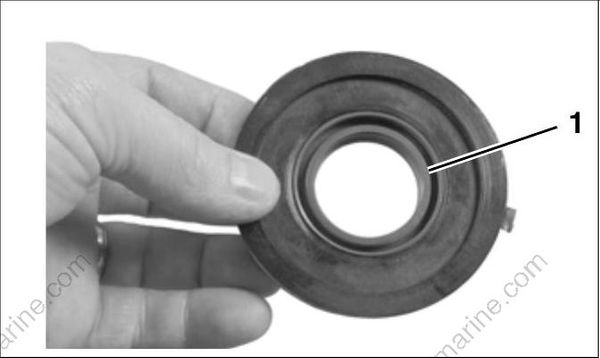
- Seal lip 002037
Lubricate a new lower seal housing O-ring with Triple-Guard grease and place the O-ring on the lower housing.
Lubricate seal lip with Triple-Guard grease and place lower seal housing on crankshaft.
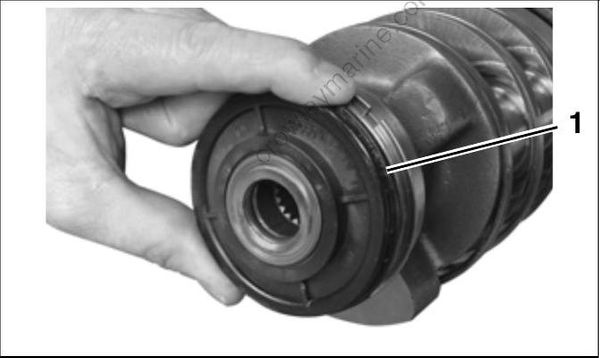
- O-ring 005280
Pistons and Connecting Rods
IMPORTANT: It is very important that the pistons in this engine are oriented correctly.
New pistons are stamped “PORT” or “STBD,” and “EXH.” These markings should be oriented to the exhaust side (center) of the block. As another reference, the splash bowl on the dome of the piston will be located toward the flywheel and opposite the exhaust port.
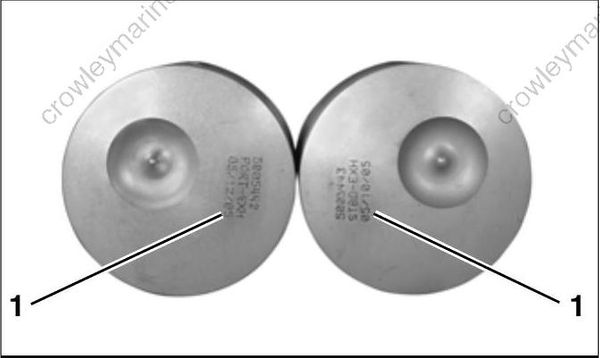
- Stamped markings 005283
IMPORTANT: It is also very important that the connecting rods are installed with the alignment dots and the diagonal oil hole facing up, toward the flywheel.
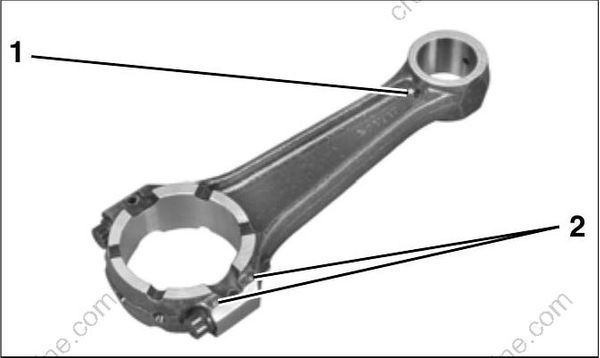
- Oil hole 002055
- Raised dots
Apply Needle Bearing Grease to the wrist pin bearings. Install the bearings in the wrist pin bore.
Align bearings with Wrist Pin Bearing Tool, P/N 336660.
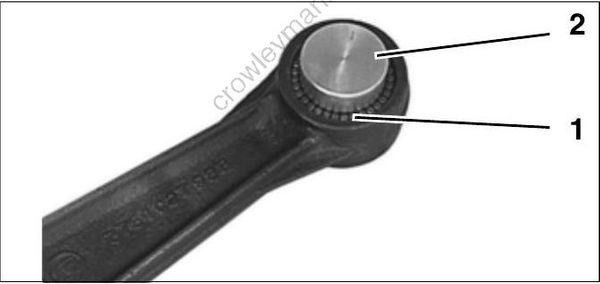
- Wrist pin bearings 31794
- Tool, P/N 336660
Place the two wrist pin thrust washers on the tool with flat side of the washers facing out.
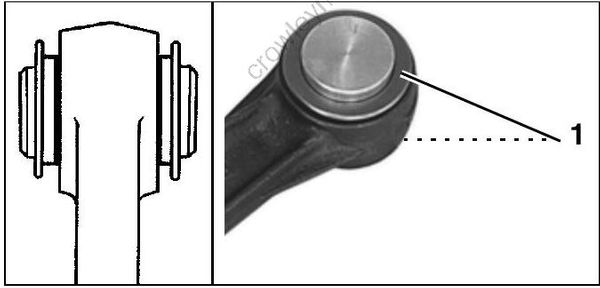
- Wrist pin thrust washers DR3480 31793
Oil the wrist pin bore and wrist pin. Place connecting rod, with bearings, washers, and tool, into the piston with the alignment dots facing the top of the piston.
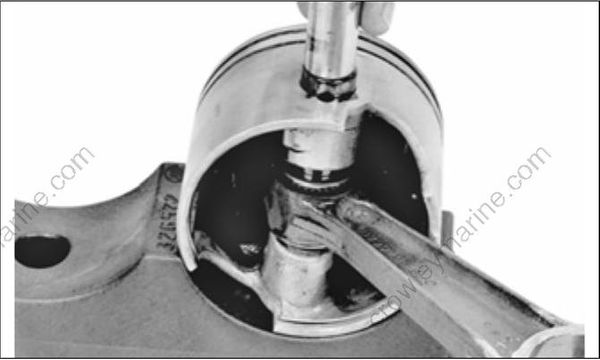
46521
Install wrist pin through piston and connecting rod, pushing bearing tool out through the piston.
Use Wrist Pin Cone, P/N 318600, and Driver, P/N 318599, to install new wrist pin retaining rings
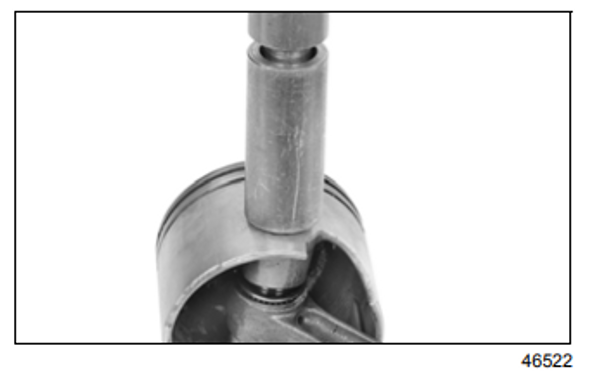
46522
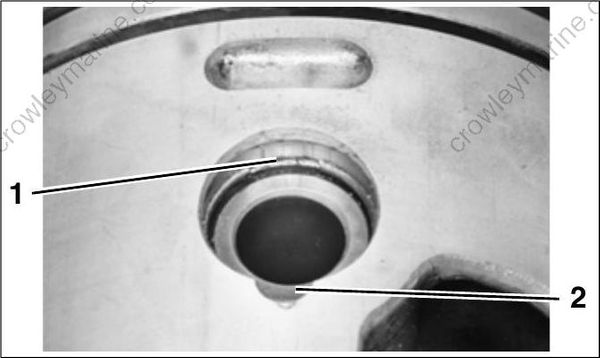
- Gap of retaining ring 46523
- Notch in piston
Repeat steps for each piston.
Installing Pistons
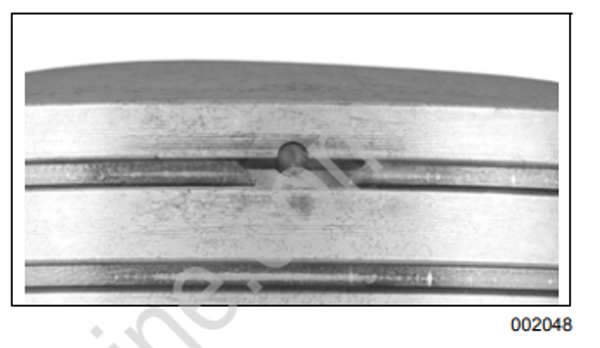
When all pistons and connecting rods are assembled, install piston ring sets. Be sure rings are installed in the cylinder used to test ring end gap.
002048
IMPORTANT: Before continuing, make sure that all Gel-Seal II has been removed from the cylinder block and crankcase mating flanges. If traces of hardened Gel-Seal II are left, main bearings could be misaligned. Refer to CLEANING on p. 247.
Coat pistons, rings, cylinder walls, and Ring Com pressor, P/N 336314 (P/N 336313 for oversize pistons), with outboard lubricant.
Center connecting rod in piston and locate piston rings on dowel pins. Place appropriate ring com pressor on piston.
Slide piston and rod assembly into the correct cylinder, as marked during disassembly. Guide connecting rod through cylinder block to avoid scratching cylinder wall.
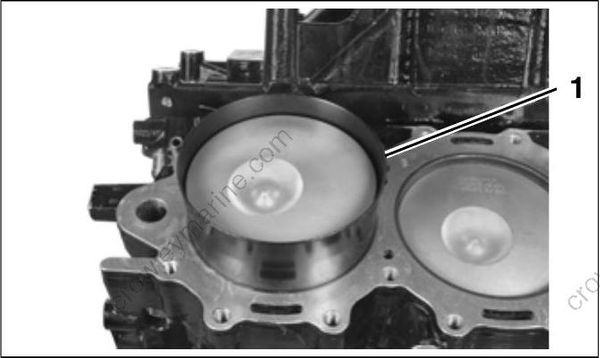
- Ring compressor 005284
Repeat steps for each piston.
Cylinder Head
Install a new thermostat seal in cylinder head with side marked “TO CYL HEAD” facing toward thermostat.
Refer to THERMOSTAT SERVICING on p. 233 prior to installing cylinder heads.
Lightly lubricate new cylinder head O-rings with Triple-Guard grease and install in cylinder block.
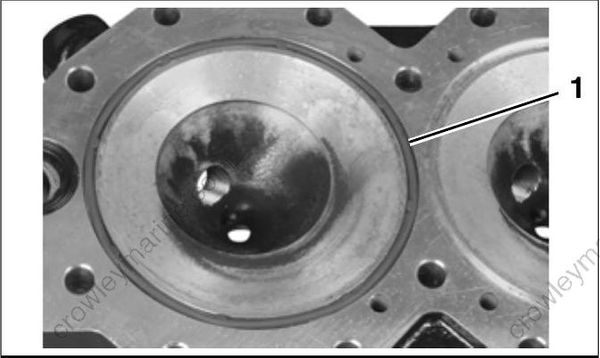
- O-Ring 005286
If it has been removed, apply soapy water to water dam and insert into block.
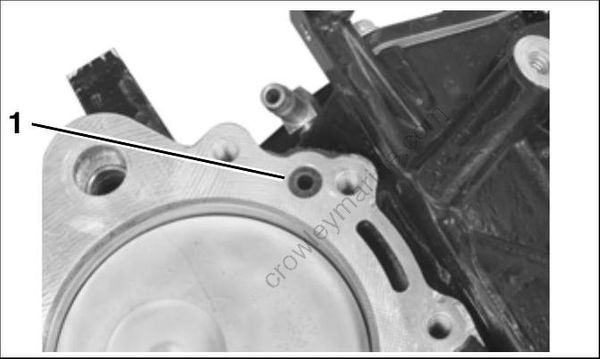
- Water dam 005287
005287 Apply a 1/16 in. (2 mm) bead of RTV adhesive around each water passage on the block and cylinder head as shown. Apply adhesive with a brush around thermostat seat area on block.
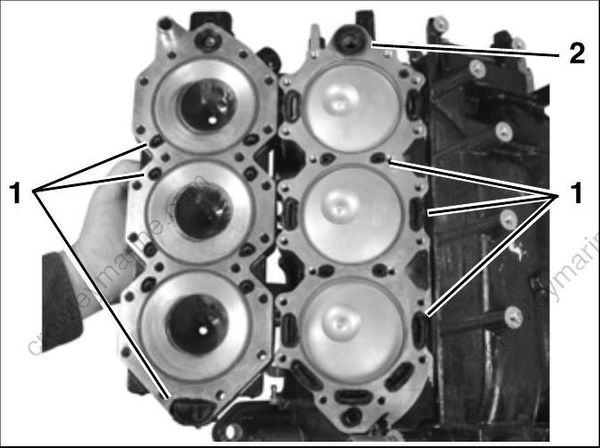
RTV adhesive (24 locations) 005288
Thermostat seat area
Install cylinder head. Apply outboard lubricant to threads and install the cylinder head screws. Following sequence on cylinder head, torque all
screws in stages to 168 to 192 in. lbs. (19 to 21.7 N·m).
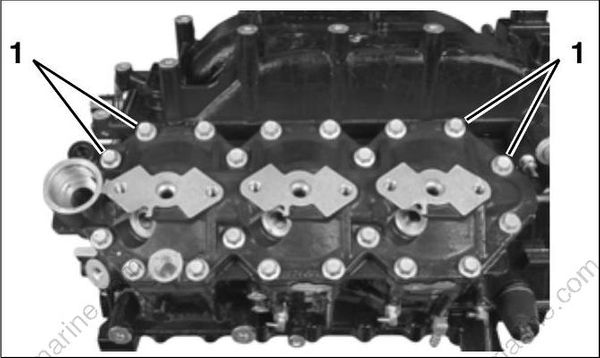
- Cylinder head screws (28 on V4; 40 on V6) 005289
Repeat steps for opposite cylinder head.
*Crankshaft and Connecting Rods8
Rotate cylinder block so crankcase mating flange is facing up.
Apply Gasket Sealing Compound_ to lower oil seal groove in cylinder block. DO NOT put any sealer in upper seal groove.
Check that main bearing alignment dowel pins are seated in the block.
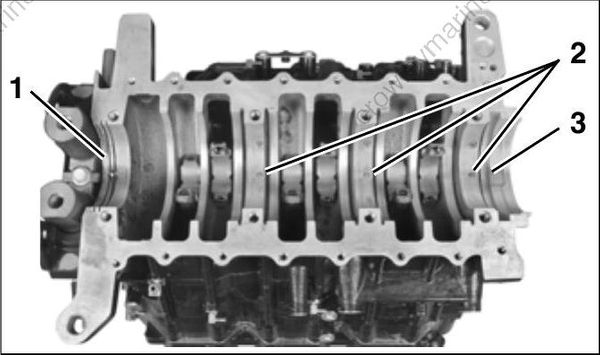
- Gasket Sealing Compound 005290
- Dowel pins
- No sealer here
Thoroughly clean upper seal area of the crank shaft. Install new upper seal on crankshaft. Do not
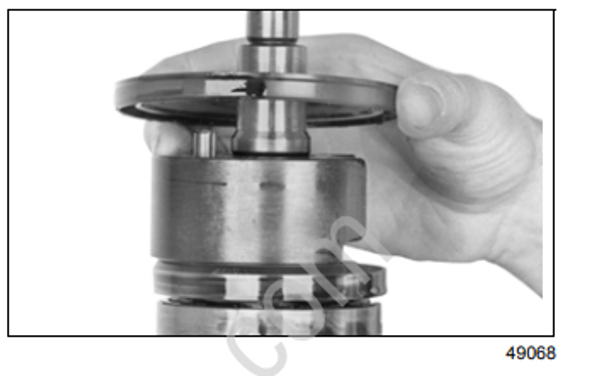
49068
Push all pistons to the top of cylinders. Remove numbered connecting rod caps.
Gently lower crankshaft into place.
• Orient all crankcase seal ring gaps facing up.
• Align tab on lower bearing seal housing with hole in crankcase.
• Align upper oil seal in groove.
• Locate each main bearing on its dowel pin. A mark placed on the bearing race opposite the
dowel pin hole will help in the alignment process.
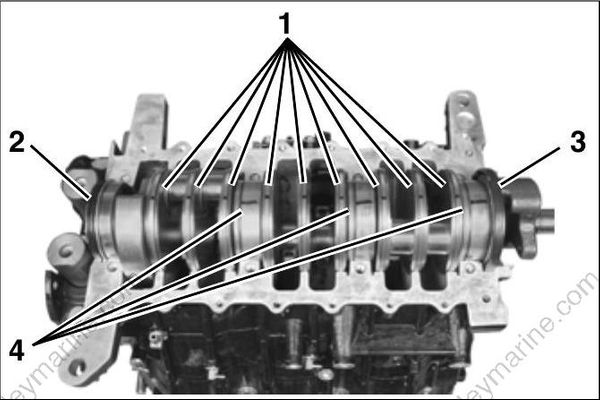
- Gaps (up) 005291
- Lower seal housing
- Upper oil seal
- Alignment marks
Lubricate each crankpin and bearing assembly
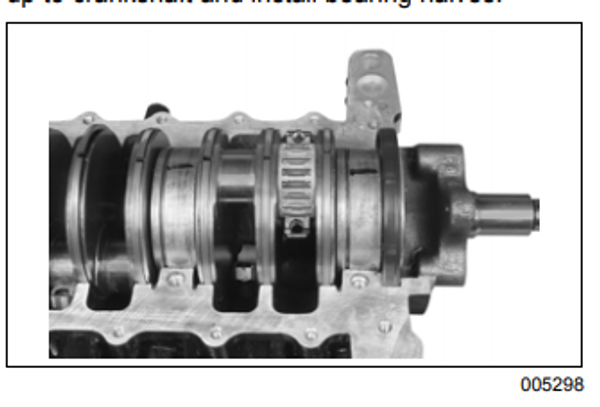
005298
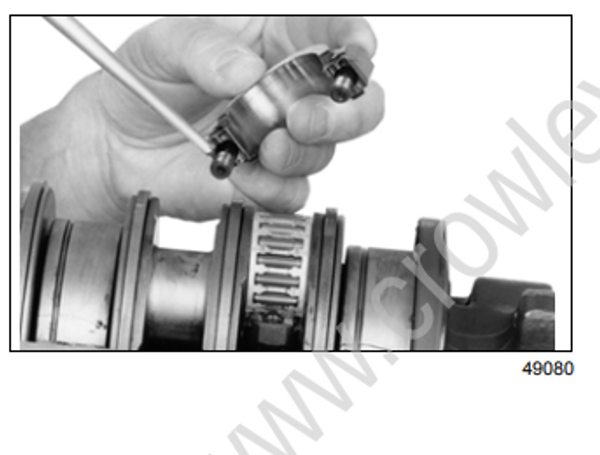
Lubricate rod cap screw threads and under screw head mating surface with outboard lubricant. Align dot on rod cap with dot on the connecting rod. Install rod cap screws finger tight (NO MORE than
49080
IMPORTANT: Be sure alignment dot on rod cap matches dot on rod and that both dots face fly wheel.
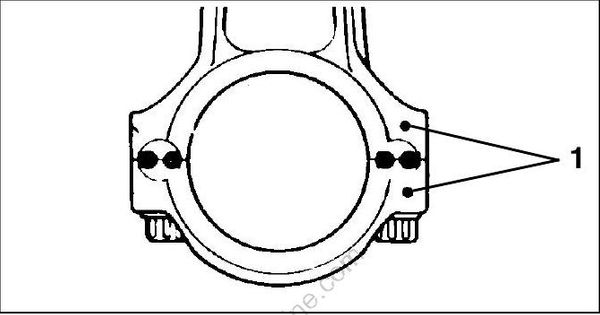
- Alignment dots 53628
IMPORTANT: Torquing the screws without Alignment Fixture, P/N 396749, or using an incorrect procedure could cause permanent damage to the connecting rod and crankshaft. To maintain accurate torque values, keep torque wrench extension length to a minimum.
Install Rod Cap Alignment Fixture, P/N 396749, before tightening rod cap screws. Align the flat marked “SET” on the rod engagement stop with the arrow on the frame. Position stop at the center setting (one line showing). Rotate adjustment knob 180° to lock in position.
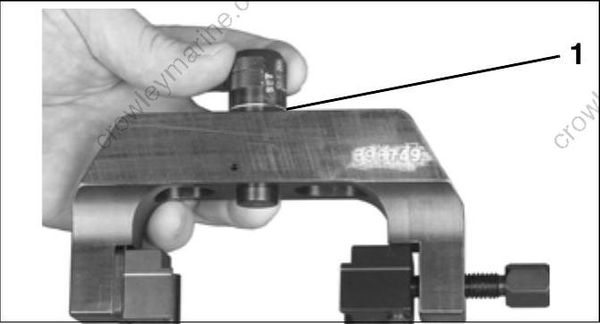
- Center position, one line showing 002484
Secure restraining jaw “C” and forcing jaw “D” to frame.
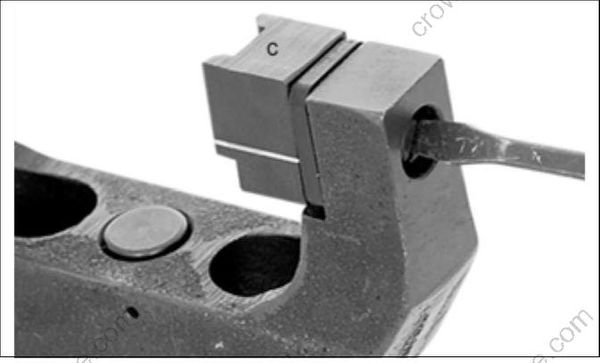
21591c
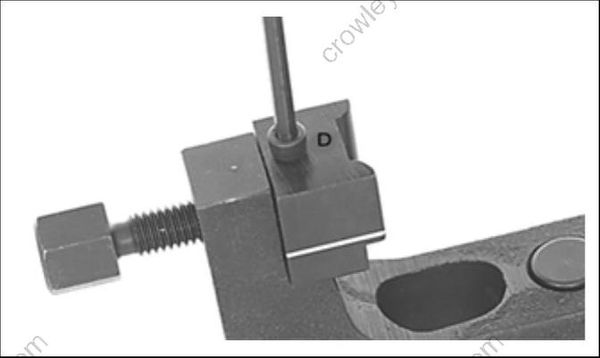
Restraining Jaw “C” 21591c
Apply a light coat of outboard lubricant to the corners of the connecting rod and rod cap. Place frame on connecting rod using the following procedure:
• Position frame onto the connecting rod so the contact area of the jaw is centered on the side of the rod.
• Tighten forcing screw until jaws contact connecting rod.
• Slide frame down until adjustment stop contacts the rod cap. The groove lines on the jaws must be centered on the rod/crankpin diameter.
• Tighten the forcing screw to a torque of 14 to 16 in. lbs. (1.6 to 1.8 N·m).
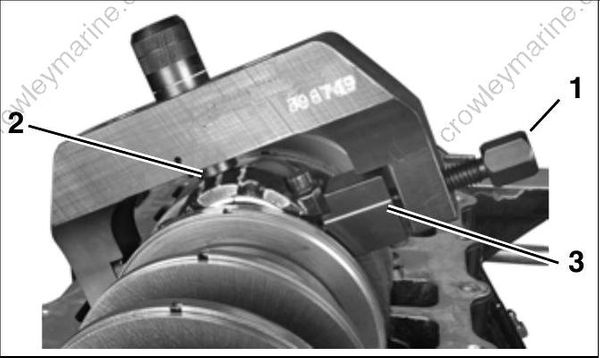
- Forcing screw 005297
- Adjustment stop
- Groove line
IMPORTANT: Make sure that frame is squarely in position and that rod and cap are aligned. Loosen both rod cap screws one-quarter turn.
Use Torquing Socket, P/N 331638, to tighten rod
cap screws in three stages:
• Apply an initial torque of 40 to 60 in. lbs. (5 to 7 N•m) to both rod cap screws.
• Torque screws to 14 to 16 ft. lbs. (19 to 21.7 N•m).
• Apply a final torque of 30 to 32 ft. lbs. (41 to 43 N•m).
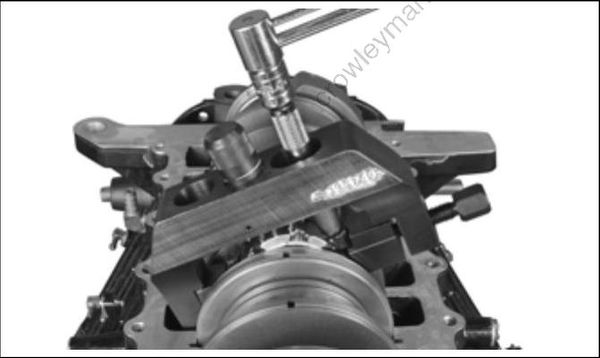
005299
Loosen forcing screw and remove the frame.
Test at least three corners of the rod and cap joint
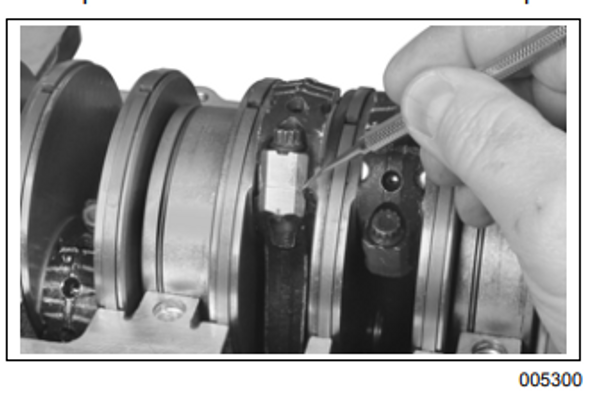
005300
Repeat steps for remaining connecting rods.
Crankcase
Thoroughly clean and degrease the mating flanges of the crankcase and cylinder block with a non-petroleum based solvent, such as isopropyl alcohol or acetone, and let air dry.
IMPORTANT: DO NOT allow solvent to get on internal components. Clean only the mating flanges.
Apply Gasket Sealing Compound_ to lower oil seal groove in crankcase. DO NOT put any sealer in upper seal groove.
Use a small brush to dab a thin, even coat of Gel- Seal II sealant to the crankcase mating flange.
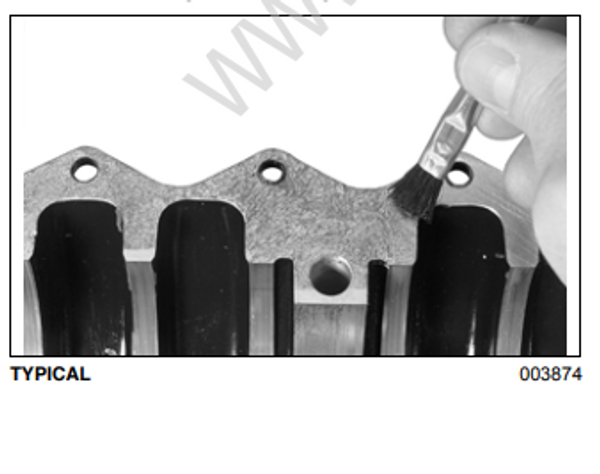
TYPICAL 003874
IMPORTANT: Gel-Seal II has a shelf life of at least one year when stored at room temperature. Test the Gel-Seal II or replace it if the age of the tube cannot be determined. Using old Gel-Seal II could cause crankcase air leaks.
IMPORTANT: If Locquic Primer is used, crank case halves must be assembled and tightened within ten minutes after the Gel-Seal II has been applied.
Lower the crankcase into place. Confirm that upper oil seal and lower seal housing are seated correctly in grooves.
Apply outboard lubricant to the main bearing screws and install screws finger tight.
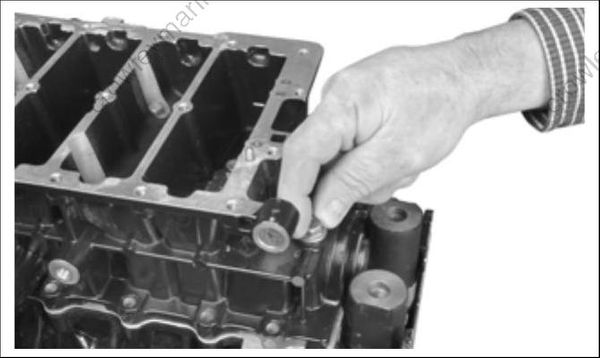
005308
When the crankcase is seated, install and firmly seat the crankcase taper pin.
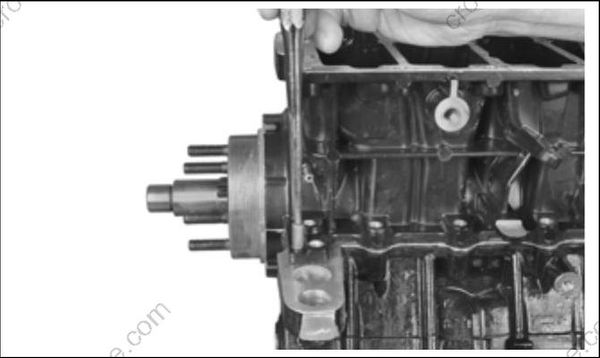
005307
Torque main bearing screws in stages to 31 to 35 ft. lbs. (42 to 47.5 N•m). Begin with the center screws and work outward in a spiral pattern.
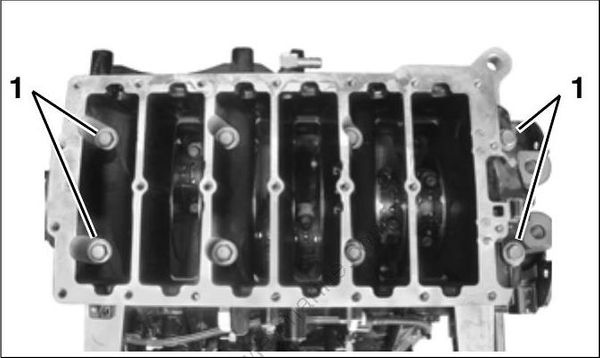
- Main bearing screws (6 on V4; 8 on V6) 005313
Apply Triple-Guard grease to crankcase flange screws. Install screws and torque to 60 to 84 in. lbs. (7 to 9.5 N•m).
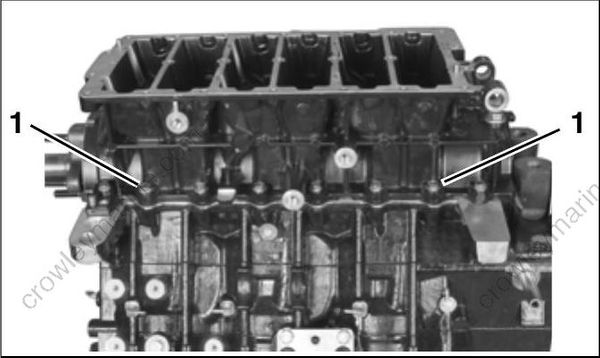
- Flange screws (12 on V4; 16 on V6) 005306
Test that the crankshaft spins freely without bind ing.
IMPORTANT: After powerhead has been assembled, allow at least two hours for Gel-Seal II to cure before running outboard.
*General8
Connect all crankcase recirculating hoses. Refer to Recirculation Hose Routings and Check
Valve Diagrams – V4 on p. 213, Recirculation Hose Routings and Check Valve Diagrams –
V6 on p. 211, or POWERHEAD VIEWS on p. 266. Install pressure valve assembly. Refer to PRESSURE RELIEF VALVE SERVICING on p. 233. Install the throttle body and reed plate assemblies. Refer to INTAKE MANIFOLD on p. 196.
Lubricate shift linkage bosses at the base of the crankcase with Triple-Guard grease. Insert bushings into bosses.
Apply Triple-Guard grease to the shaft of the shift lever assembly. Guide shaft through bushings in crankcase.
Install shift rod lever and tighten retaining screw 60 to 84 in. lbs. (7 to 9.5 N •m).
Apply Triple-Guard grease to shoulder of shift arm screw and Nut Lock to threads. Install arm, screw, and washer and torque screw to 120 to 144 in. lbs. (14 to 16 N•m).
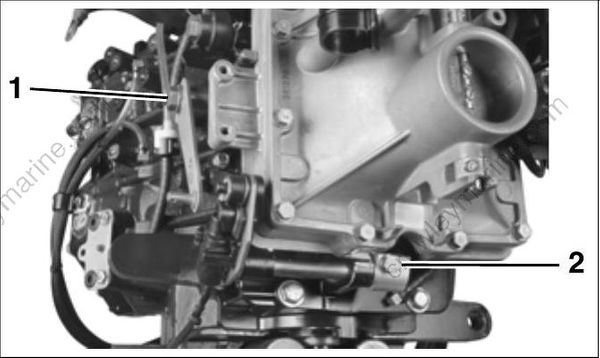
- Throttle lever spring 005259
Apply Nut Lock to threads of throttle lever screw. Insert spring into cavity of throttle lever. Install lever, screw, and washer on crankcase and hook spring on rib as shown. Torque screw to 120 to 144 in. lbs. (14 to 16 N·m).
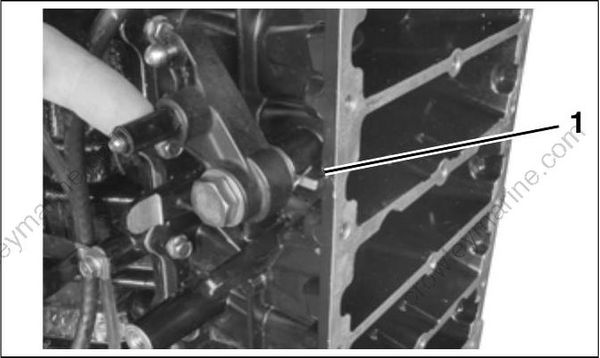
- Throttle cam screw 005293
Apply Nut Lock to threads of throttle cam screw. Install cam, screw, and washer and torque screw to 120 to 144 in. lbs. (14 to 16 N·m).
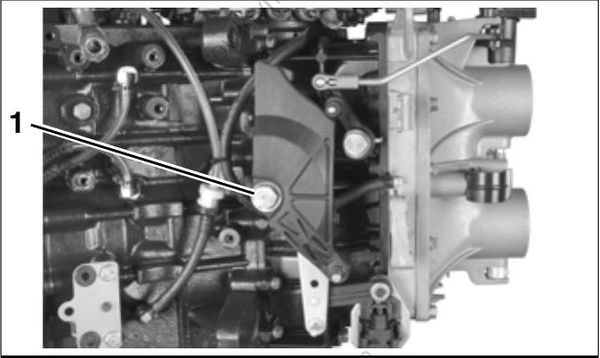
IMPORTANT: Do not lubricate throttle levers or shoulder screws.
Install ignition coils and fuel injectors. Refer to Fuel Injectors on p. 193.
IMPORTANT: All injectors must be reinstalled in their original location. Improper injector installation can result in powerhead failure.
Install oil pump, rear oil manifold, and oil injection hoses. Refer to OIL COMPONENT SERVICING on p. 222.
Install flywheel and stator. Refer to FLYWHEEL AND STATOR SERVICING on p. 154.
Install electrical harness with flywheel cover base, starter solenoid, and trim relay module, then install EMM.
Install fuel pump assemblies, fuel manifolds, and filter. Refer to FUEL COMPONENT SERVICING on p. 189.
Install the electric starter. Refer to Starter Installation on p. 167.
To prevent fire and explosion hazard, make sure all electrical and ignition wiring is routed and clamped in original positions.
